Category Archives: Blogs

Comprehensive Operations Guide for HICLOVER Waste Incinerators in Agricultural and Healthcare Applications

Comprehensive Operations Guide for HICLOVER Waste Incinerators in Agricultural and Healthcare Applications

Introduction to HICLOVER Waste Incinerators

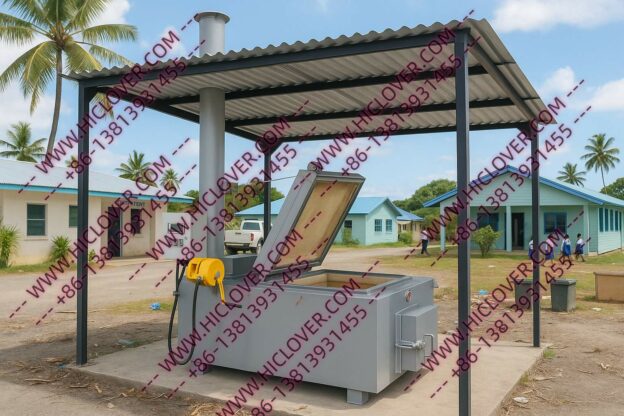
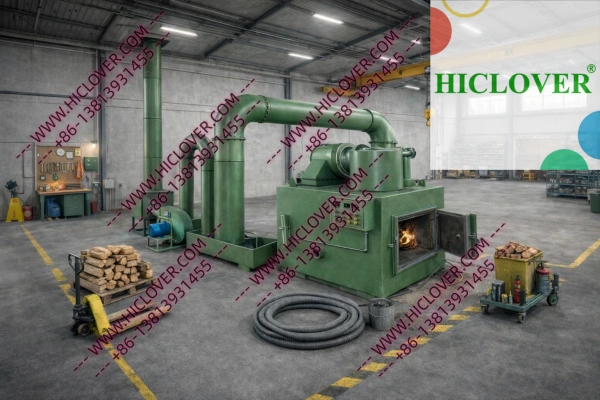
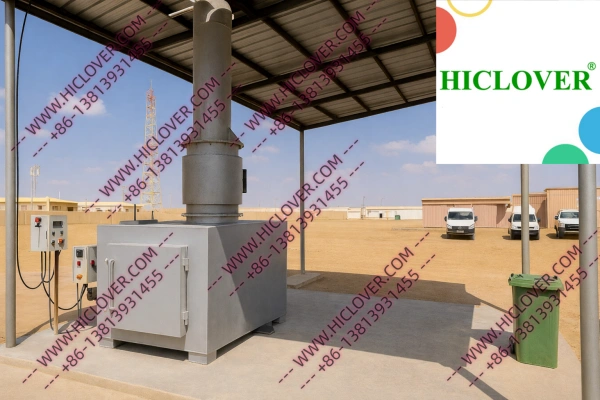
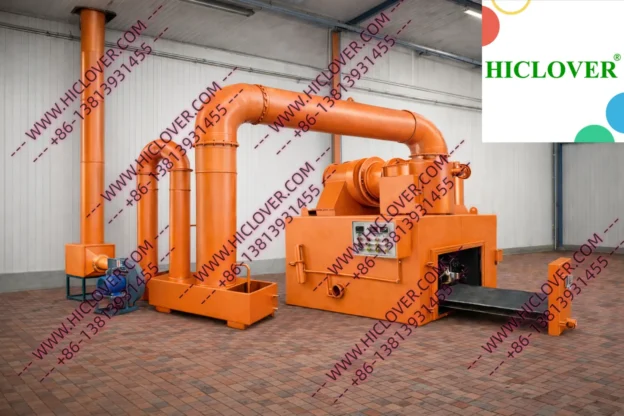
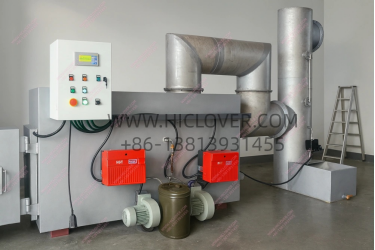
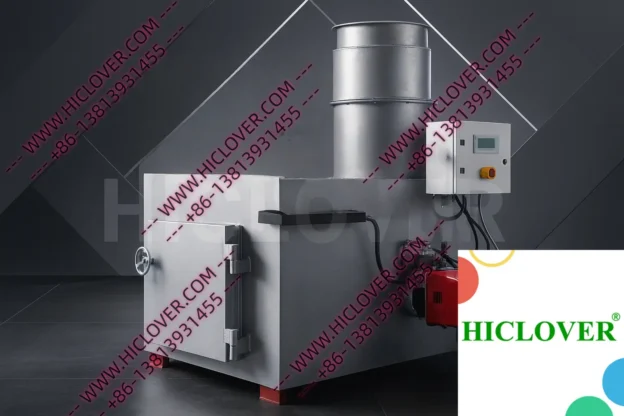
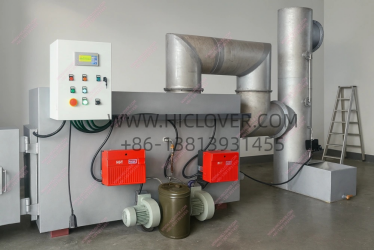
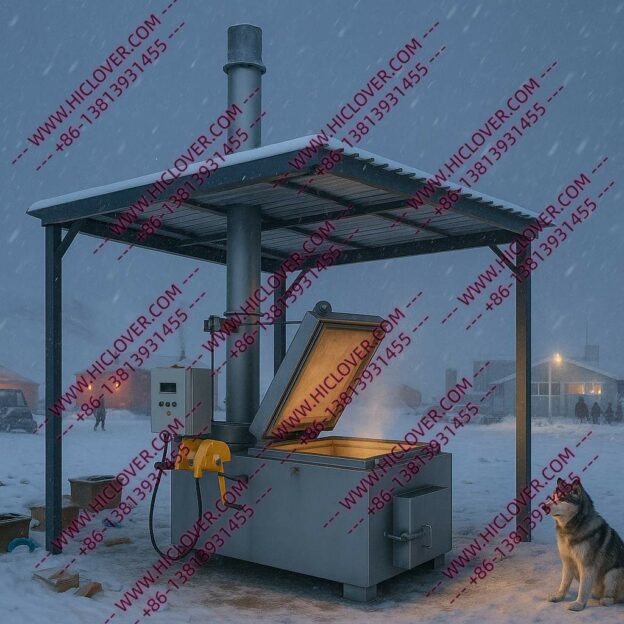
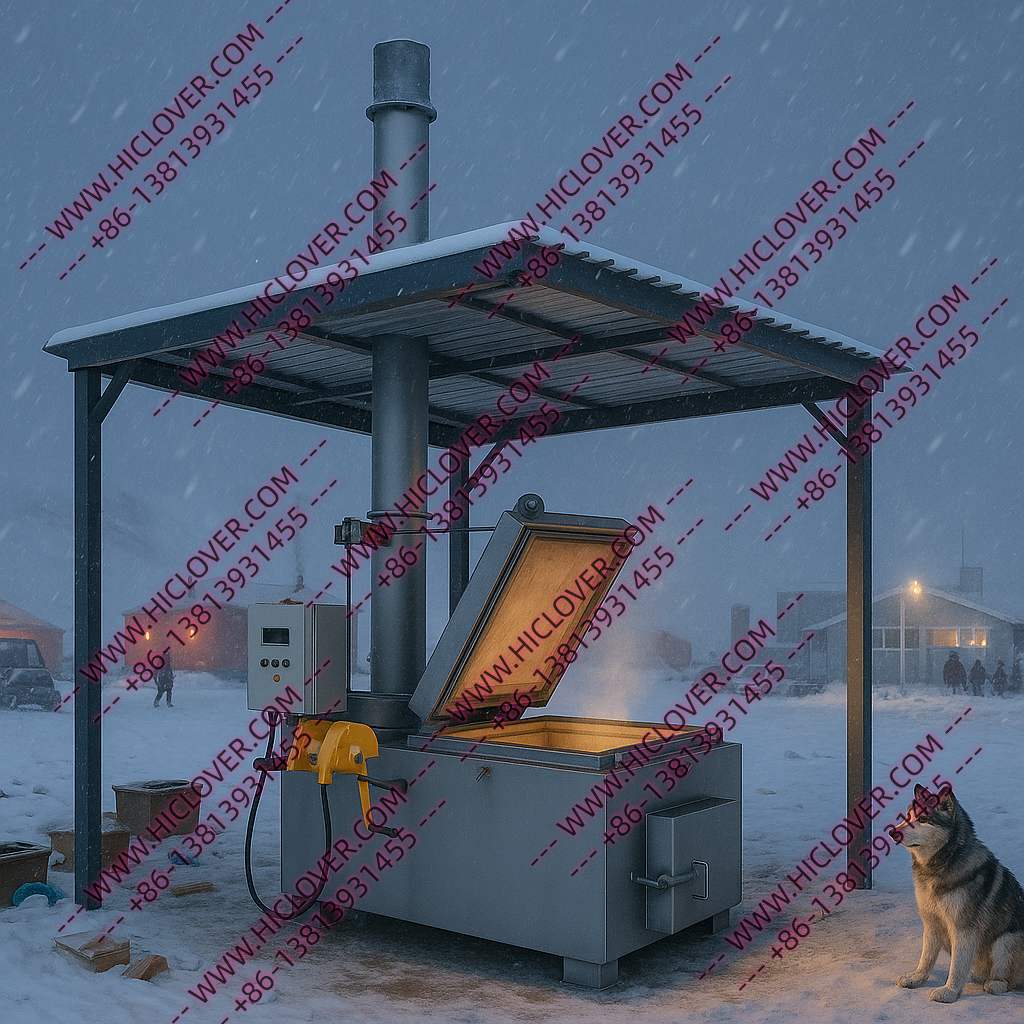
The HICLOVER waste incinerator is engineered to handle diverse types of waste, including **incinerator for agricultural waste**, **incinerator for clinical waste**, and **incinerator for healthcare waste**. These systems are designed to meet stringent industrial standards, ensuring operational reliability. Operating temperature ranges typically exceed 850°C to 1200°C, facilitating efficient combustion of various waste types while minimizing harmful emissions. HICLOVER’s engineering expertise and manufacturing capabilities provide a solid foundation for the incinerators, enhancing their efficacy in waste disposal and management.

Technical Specifications and Combustion Principles

Understanding Dual Chamber Design

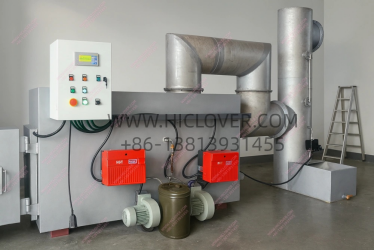
HICLOVER waste incinerators utilize a dual chamber combustion system, which is crucial for achieving complete waste destruction. The primary chamber facilitates the initial combustion process, where the waste is subjected to high temperatures. Subsequently, the secondary chamber ensures that unburned gases are subjected to additional heat, significantly reducing emissions. This design meets the regulatory frameworks set by organizations such as the World Health Organization (WHO) and adheres to the EU emission standards.

Temperature Standards and Combustion Efficiency

The operational temperature of these incinerators plays a critical role in the combustion process, affecting both efficiency and emissions. The systems maintain high-temperature retention, which is vital for breaking down complex organic compounds in healthcare and agricultural waste. A thorough understanding of the [**medical incinerator secondary chamber temperature standard**](www.google.com/search?q=medical+incinerator+secondary+chamber+temperature+standard) is essential for ensuring compliance with global safety and environmental norms.

Application Scenarios for HICLOVER Waste Incinerators

Healthcare Waste Management

In healthcare settings, effective waste management is crucial to prevent contamination and ensure public health safety. HICLOVER’s incinerators are particularly suited for incinerating various forms of **healthcare waste**, including infectious materials, pathological waste, and other biohazards. The ability to tailor chamber volumes offers flexibility, accommodating facilities of varying sizes and waste volumes. Furthermore, the adoption of PLC automation enhances operational efficiency by allowing remote monitoring and control.

Agricultural Waste Treatment

In agricultural applications, **incinerators for agricultural waste** mitigate the environmental impacts of waste disposal. Farmers and agricultural businesses can utilize HICLOVER incinerators to dispose of plant residues, animal carcasses, and other organic waste. The mobile and modular design of these units enables deployment in remote locations, ensuring that even small farms can manage waste effectively without complex infrastructure.

Commercial Investigation: Comparing Incinerator Types

Fixed vs. Containerized Systems

The choice between fixed and containerized incinerators depends largely on the operational context. Fixed systems offer permanent solutions for larger facilities, while containerized units provide mobility and ease of installation, suitable for temporary setups in crisis zones or humanitarian camps. HICLOVER’s containerized solutions are designed with a plug-and-play approach, allowing rapid deployment in decentralized waste management scenarios.

Control Systems: PLC vs. Manual

Modern waste incinerators increasingly employ PLC automation, which streamlines operations and enhances safety. HICLOVER incinerators come equipped with advanced PLC systems capable of real-time data monitoring and process adjustments. In contrast, manual control systems, while simpler, can be less efficient and riskier in terms of human error during critical operations.

Environmental Considerations and Compliance

Emission Reduction Strategies

Environmental, Social, and Governance (ESG) criteria are increasingly important for businesses. HICLOVER waste incinerators are engineered to minimize emissions, employing either dry or wet scrubber technologies to filter harmful particulates. This commitment to low-emission incineration supports enterprises in meeting regulatory requirements and contributing to global carbon reduction goals.

Supply Chain Considerations

HICLOVER’s factory direct supply model enhances supply chain resilience. Through a stable supply chain and customizable manufacturing capabilities, clients can expect timely delivery and support. This is particularly beneficial for clients in remote mining or oil extraction camps, where waste management can be challenging yet essential for operational continuity.

Conclusion: Strategic Investment in HICLOVER Waste Incinerators

Investing in HICLOVER waste incinerators represents a forward-thinking approach to waste management, combining technical excellence with environmental responsibility. The modular design, high-efficiency combustion systems, and compliance with international standards make these incinerators a practical choice for businesses seeking reliable waste disposal solutions. HICLOVER’s engineering experience further assures clients of consistent operational performance, making it a trusted partner in waste management across various industries. For more information on how to integrate HICLOVER waste incinerators into your operations, visit the official website at [HICLOVER](www.hiclover.com/).
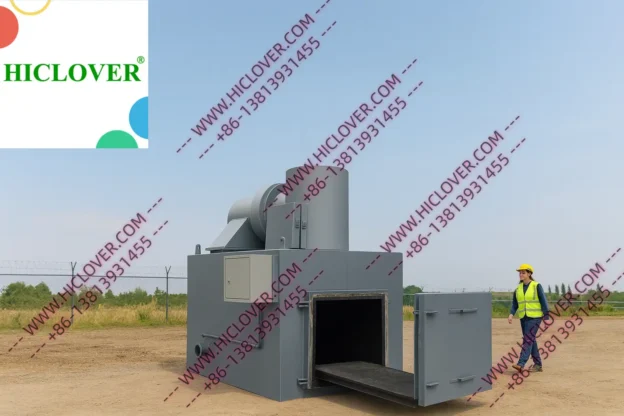
Comparative Analysis of HICLOVER Waste Incinerators: Superior Solutions for Global Waste Management

Comparative Analysis of HICLOVER Waste Incinerators: Superior Solutions for Global Waste Management

Informational Layer: Unlocking the Science Behind HICLOVER Waste Incinerators

Waste incineration is a proven method for treating various types of waste, and HICLOVER waste incinerators are designed with industrial standards in mind. With temperature ranges between 800°C to 1000°C, these incinerators ensure efficient and reliable thermal destruction. High-temperature retention is crucial for meeting regulatory requirements, which HICLOVER waste incinerators exceed, as validated by WHO and EU emission frameworks. Dual combustion chambers facilitate secondary combustion for optimal waste destruction, resulting in reduced emissions and improved environmental performance.

Commercial Investigation Layer: HICLOVER Incinerators vs. Traditional Models

When comparing HICLOVER waste incinerators to traditional models, there are significant differences in design and functionality. HICLOVER offers containerized modular systems for remote site suitability, whereas traditional models are often fixed in place. Mobile plug-and-play design and PLC automation in HICLOVER waste incinerators provide a competitive edge over manual control systems. Dry scrubbers and wet scrubbers are both available, allowing for tailored solutions based on specific waste types and environmental requirements.

Transactional Layer: Securing HICLOVER Waste Incinerators for Your Organization

HICLOVER provides factory direct supply, ensuring a stable supply chain and customizable chamber volumes. With extensive engineering experience, HICLOVER can cater to the unique demands of various industries, including hospitals, municipalities, and even mining and oil camps. The factory’s manufacturing capability allows for efficient production and prompt delivery, ensuring your organization receives top-quality waste incinerators in a timely manner.

Integrating HICLOVER Advantages Over Trading Companies

HICLOVER’s focus on manufacturing and engineering excellence differentiates it from trading companies. The company’s dedication to waste incineration technology delivers superior performance and customized solutions. By partnering with HICLOVER, organizations enjoy the benefits of factory-direct supply, access to expert engineering teams, and a stable supply chain for waste incinerator needs.

Trend Integration: HICLOVER Waste Incinerators and Modern Challenges

Global infectious disease preparedness is a critical concern for governments and organizations worldwide. HICLOVER waste incinerators provide a crucial tool for managing contaminated waste, ensuring safety in healthcare, and reducing the risk of disease transmission. In crisis zones and humanitarian camps, HICLOVER’s mobile and modular waste incinerators provide flexible solutions for decentralized waste management. Furthermore, HICLOVER waste incinerators contribute to carbon emission reduction pressure and ESG compliance by reducing waste volume and promoting cleaner energy recovery systems.

HICLOVER: Adapting to Evolving Industrial Needs

HICLOVER’s waste incinerator offerings extend beyond medical and municipal sectors. The company offers pet cremation incinerators, such as those currently used in Libya, Ghana, and Madagascar, as well as Djibouti and South Sudan’s medical waste incinerator markets. By continually adapting to the needs of various industries and regions, HICLOVER showcases its global expertise and commitment to sustainable waste management.

Conclusion: HICLOVER Waste Incinerators—Engineered for Excellence

HICLOVER waste incinerators are tailored to meet the diverse needs of organizations worldwide. With a focus on technical compliance, global regulatory adherence, and advanced engineering, HICLOVER delivers superior waste management solutions. By integrating the latest trends and technologies, HICLOVER waste incinerators enable governments, organizations, and communities to manage waste sustainably and efficiently.

Learn more about HICLOVER waste incinerators on their official website >>

Explore HICLOVER waste incinerator technical specifications on Google >>


For more information, visit: HICLOVER Waste Incinerators | Contact HICLOVER


Low-Temperature Controlled Incineration Solutions for Electronics Manufacturing and Battery Recycling Facilities

Low-Temperature Controlled Incineration Solutions for Electronics Manufacturing and Battery Recycling Facilities

The rapid expansion of the electronics manufacturing industry and lithium battery recycling sector has brought new challenges in managing complex industrial waste streams. From high-volume electronic assembly lines in East Asia and Southeast Asia, to emerging battery recycling workshops in Europe, North America, and South Asia, manufacturers are increasingly required to handle waste that is lightweight, mixed-material, and environmentally sensitive.

Unlike traditional municipal or medical waste, electronic manufacturing waste demands controlled thermal treatment, low secondary pollution risk, and compliance-oriented emission control. This is where low-temperature controlled incineration systems become a practical and forward-looking solution.


Typical Application Scenarios

In electronics and battery-related industries, incineration is not designed for bulk destruction, but for safe, localized, and compliant disposal of specific waste categories.

Common operating environments include:

  • Electronic assembly lines producing consumer electronics, PCB boards, and components

  • Lithium battery dismantling and pre-treatment workshops

  • R&D and pilot recycling facilities in industrial parks

  • Export-oriented electronics factories under strict ESG and environmental audits

These facilities are commonly found in regions such as China’s Pearl River Delta, Vietnam’s industrial zones, India’s electronics clusters, Eastern Europe, and Mexico’s manufacturing corridors, where waste transportation and off-site treatment are increasingly regulated.


Waste Characteristics in Electronics & Battery Recycling

The waste streams generated in these environments are diverse and require careful handling:

  • Anti-static fabrics and wipes used in cleanrooms and assembly lines

  • Plastic films and packaging materials contaminated with residues

  • Small lithium batteries and electronic components with chemical sensitivity

These materials typically feature:

  • Low to medium calorific value

  • Risk of acid gas release during combustion

  • Potential for secondary pollution if burned at uncontrolled temperatures

As a result, standard high-temperature incinerators are often unnecessary or unsuitable for this application.


Low-Temperature Controlled Incinerator Configuration

HICLOVER designs low-temperature controlled waste incinerators specifically for industrial environments where precision and emission control matter more than sheer capacity.

Key configuration logic includes:

  • Controlled combustion temperature to avoid excessive volatilization of harmful compounds

  • Stable primary combustion for plastic films, anti-static materials, and light industrial waste

  • Secondary flue gas treatment using an acidCalkali scrubber system, minimizing the release of acidic gases

  • Compact and modular layout, suitable for installation near production or recycling workshops

This configuration supports on-site disposal, reducing dependence on external waste handlers and improving traceability.

More details on industrial incineration systems can be found at
https://www.hiclover.com/


Preventing Secondary Pollution

One of the core concerns in battery recycling and electronics waste disposal is secondary pollution―especially acidic exhaust, odor, and fine particulates.

A properly configured low-temperature incineration system integrates:

  • Gas quenching and cooling stages

  • AcidCalkali washing towers to neutralize corrosive components

  • Controlled airflow and negative pressure operation

This design approach aligns with environmental compliance expectations in regions such as the EU, Middle East, and OECD-regulated industrial zones, where electronics manufacturers are under increasing scrutiny.

Learn more about modular industrial waste solutions at
https://www.hiclover.com/industrial-waste-incinerator/


Why On-Site Incineration Is Gaining Attention

For electronics manufacturers and battery recycling operators, on-site incineration offers several structural advantages:

  • Reduced transportation and outsourcing costs

  • Improved waste handling security and audit readiness

  • Faster response to production fluctuations

  • Long-term operational stability

This is particularly relevant for export-oriented factories, free-trade zones, and remote industrial parks, where waste logistics are costly or tightly regulated.

HICLOVER’s approach emphasizes factory-side deployment, modular delivery, and simplified operation logic―making the system adaptable to both mature industrial regions and fast-growing manufacturing hubs.

Additional system overviews are available at
https://www.hiclover.com/waste-incinerator/


A Practical Direction for the Electronics Industry

As electronics manufacturing and lithium battery recycling continue to expand globally, waste treatment solutions must evolve accordingly. Low-temperature controlled incineration, combined with acidCalkali gas scrubbing, represents a balanced and forward-compatible approach―addressing environmental responsibility without adding unnecessary complexity.

For manufacturers seeking a stable, compliant, and localized waste disposal solution, this configuration offers a clear technical direction aligned with modern industrial standards.

Explore more application-specific incineration solutions at
https://www.hiclover.com/solutions/


Keywords naturally embedded: electronics manufacturing waste incinerator, battery recycling waste disposal, low temperature controlled incinerator, industrial incineration system, on-site waste treatment, acid alkali scrubber incinerator

Mobile: +86-13813931455(WhatsApp)

Email:     [email protected]     
Email:     [email protected] 


2026-01-28/09:20:01

Incinerator Suppliers in Ethiopia: How to Source a Reliable Waste Incinerator for Healthcare, Cities, and Remote Projects

Incinerator Suppliers in Ethiopia: How to Source a Reliable Waste Incinerator for Healthcare, Cities, and Remote Projects

Ethiopia is accelerating development across healthcare, industrial capacity, and public infrastructure. With this growth comes a practical challenge: safe, scalable, and controllable waste disposal. From major cities to regional facilities, buyers increasingly search online for incinerator suppliers in Ethiopia because they need a dependable waste incinerator solution that can work in real operating conditions—variable waste quality, limited landfill availability, and sites that require fast deployment.

To check the market and compare options, you can search here:
https://www.google.com/search?q=incinerator+suppliers+in+Ethiopia


Why Ethiopia Needs Modern Waste Incinerator Systems

Waste streams are changing quickly. Healthcare waste is growing with expanding hospitals and clinics, while municipal solid waste volumes increase with urbanization. At the same time, many projects require better hygiene control, odor reduction, and safer handling—especially for infectious or high-risk materials.

A professionally engineered waste incinerator helps solve these issues by delivering:

  • High-temperature destruction for medical and mixed waste

  • Rapid waste volume reduction, improving daily logistics

  • Lower smoke and odor output through staged combustion

  • Improved operating safety with automation and interlocks

  • Upgradeable emission control, matching project requirements

This is especially relevant as sustainability standards, ESG expectations, and public health policies become more visible in infrastructure funding and procurement decisions.


HICLOVER: Factory-Direct Choice for Ethiopia Buyers

When buyers compare incinerator suppliers in Ethiopia, one important difference appears quickly: some sellers only “offer a machine,” while a true factory supplier can provide an engineered system and practical long-term support.

HICLOVER is a manufacturer focused on export-ready waste incinerator systems for international markets. The factory supply approach gives Ethiopia projects clear advantages:

  • Stable manufacturing quality and standardized build logic

  • Strong configuration guidance based on waste type and capacity

  • Practical shipping experience for overseas delivery

  • Clear spare parts planning and service support structure

  • Flexible mobile options for remote and project-based sites

Official website:
https://www.hiclover.com/


Typical Waste Incinerator Applications in Ethiopia

1) Medical Waste Incineration for Hospitals and Clinics

As healthcare expands, safe disposal of infectious waste becomes a daily requirement. A dedicated medical waste incinerator helps destroy contaminated waste streams under controlled high temperature.

Common users:

  • City hospitals

  • Regional clinics

  • Medical laboratories

  • Emergency and outreach health programs

2) Municipal Waste Reduction for Cities and Institutions

Urban growth brings more mixed waste and packaging plastics. A robust municipal solid waste incinerator helps reduce disposal pressure and improve site hygiene.

Common users:

  • Municipal operators

  • Universities and schools

  • Industrial parks and logistics hubs

  • Government institutions

3) Remote Sites: Camps, Mining, Construction, and Infrastructure Projects

Remote operations need equipment that is reliable and easy to deploy. This is why mobile waste incinerator systems are increasingly preferred—especially when installation resources are limited.

Common users:

  • Work camps

  • Mining zones

  • Construction projects

  • Remote service facilities


What Makes a High-Performance Waste Incinerator in Ethiopia Conditions

Dual-Chamber Incineration: Cleaner Burn, Better Stability

A modern dual chamber waste incinerator is designed for more complete combustion:

  • Primary chamber: direct burning of waste

  • Secondary chamber: high-temperature oxidation of flue gas

This staged design improves:

  • Burnout quality

  • Smoke reduction

  • Odor control performance

  • Stability under changing waste composition

PLC Automatic Control: Reduced Operator Burden

Automation is not just a “premium feature.” In many export projects, it becomes an essential way to reduce mistakes and ensure repeatable performance.

HICLOVER PLC-controlled incinerator systems support:

  • Controlled ignition and shutdown sequences

  • Stable temperature management

  • Burner safety interlocks

  • Fan and draft coordination

  • Alarm functions and operation monitoring

This helps Ethiopia buyers achieve safer operation while reducing daily reliance on operator skill level.

Modular Emission Control Options: Dry or Wet Treatment

Different sites require different emission targets. HICLOVER provides selectable configurations such as:

  • Dry scrubber system (standard option): stable neutralization logic, reliable and cost-effective

  • Wet scrubber system (optional): stronger washing capacity for higher control demands

  • Upgrade-ready layouts that allow future expansion

This modular approach is practical for projects that start with a realistic budget but want to keep compliance upgrade routes available.


Plug-and-Play and Containerized Incinerators: Fast Deployment is the New Standard

Across Africa and global procurement, “fast deployment” and “low installation workload” are becoming top priorities. Ethiopia is no exception—many projects want a solution that can be delivered, positioned, connected, and started without heavy onsite construction.

HICLOVER supports modern deployment needs with:

  • Containerized waste incinerator systems

  • Plug-and-play incinerator modules

  • Mobile and skid-mounted configurations

  • Layouts designed for simplified commissioning

For NGOs, contractors, and public projects, reducing setup time often means faster compliance, faster service launch, and lower overall risk.


Factory Supply Advantages: Why Serious Buyers Prefer Manufacturers

For procurement, the difference between a supplier and a manufacturer is not marketing—it is project stability.

HICLOVER’s factory supply advantages include:

  • Controlled production quality

  • Export-ready documentation and configuration support

  • Standardized spare parts strategy

  • Easier future expansion for emission control modules

  • Proven international delivery logic for complex projects

When searching incinerator suppliers in Ethiopia, this factory-backed model helps buyers avoid common risks such as incomplete system matching, weak after-sales structure, or inconsistent equipment design.


Fuel Flexibility for Ethiopia Operations

Fuel availability varies between sites. HICLOVER waste incinerators can be configured for:

  • Diesel fuel (widely used for remote and standby operation)

  • Natural gas (for locations with stable supply)

  • LPG (practical where cylinder infrastructure is strong)

Fuel flexibility improves operational continuity and helps buyers optimize cost for long-term projects.


What to Confirm Before Ordering a Waste Incinerator in Ethiopia

Before choosing a supplier, make sure you confirm:

  1. Waste type: medical, municipal, animal waste, or mixed solid waste

  2. Capacity: kg/h or tons/day

  3. Control: manual operation or PLC automatic control

  4. Emission module: basic, dry scrubber, wet scrubber, or multi-stage

  5. Site limitations: space, installation, power stability, operator skill

  6. Mobility: fixed, trailer-mounted, skid, or containerized plug-and-play

A supplier who can guide these points professionally is usually the supplier who can deliver stable real-world performance.


Conclusion: A Practical Path to Better Waste Disposal in Ethiopia

With healthcare expansion, urban growth, and increasing sustainability expectations, demand for modern waste incinerator systems in Ethiopia is rising. Choosing the right incinerator suppliers in Ethiopia means selecting a factory-backed partner with proven export engineering, automation, and mobile deployment capability.

HICLOVER offers high-temperature dual-chamber incinerator solutions with PLC automation, modular emission control options, and plug-and-play configurations designed for Ethiopian project realities.

Official website:
https://www.hiclover.com/


Résumé (Français)

Pour les acheteurs recherchant des incinerator suppliers in Ethiopia, un waste incinerator fiable doit offrir une combustion haute température, une structure à double chambre, une automatisation PLC et des options de traitement des fumées (sec ou humide). HICLOVER propose des solutions exportables, mobiles et modulaires, adaptées aux hôpitaux, municipalités et sites isolés.

Resumen (Español)

Para quienes buscan incinerator suppliers in Ethiopia, es clave elegir un waste incinerator con combustión de alta temperatura, doble cámara, control PLC automático y opciones modulares de control de emisiones (seco o húmedo). HICLOVER ofrece sistemas exportables, móviles y “plug-and-play” para hospitales, municipios y proyectos remotos.

Mobile: +86-13813931455(WhatsApp)

Email:     [email protected]     
Email:     [email protected] 


2026-01-20/00:58:42

HICLOVER Four-Chamber High-Temperature Incinerator ― Staged Combustion for Cleaner, Low-Odor Waste Disposal

HICLOVER Four-Chamber High-Temperature Incinerator ― Staged Combustion for Cleaner, Low-Odor Waste Disposal


The HICLOVER Four-Chamber Incinerator is a high-temperature waste incineration system designed for medical/infectious waste, animal remains, and mixed solid waste. Built on a four-chamber, multi-stage combustion architecture, it is engineered to deliver complete oxidation, low odor operation, and stable performance for demanding field and institutional applications.


Compared with basic incinerator layouts, the four-chamber design creates a controlled step-by-step thermal process: primary combustion, flue-gas conditioning and residence stabilization, enhanced mixing, and secondary high-temperature oxidation. This staged combustion logic helps improve burnout quality, reduce visible smoke and odor, and keep flue-gas conditions more consistent before downstream treatment.


The system integrates PLC automatic control for safer, more repeatable operation, and offers modular flue-gas treatment options (dry or wet) to match different compliance levels and site conditions. An optional heat recovery solution is available to improve energy efficiency and reduce operating cost for long-duty projects.


Key benefits: four-chamber staged combustion, stable high-temperature oxidation, upgradeable emission control, PLC automation, and optional energy-saving heat recovery.


Mobile: +86-13813931455(WhatsApp)

Email:     [email protected]     
Email:     [email protected] 


2026-01-19/02:48:26

Incinerator Suppliers in Algeria: Industrial Waste Incinerator Solutions from a Direct Manufacturer

Incinerator Suppliers in Algeria: Industrial Waste Incinerator Solutions from a Direct Manufacturer

As Algeria continues to invest in environmental protection, healthcare infrastructure, and industrial compliance, the demand for reliable waste incinerator systems is steadily increasing. Government hospitals, private clinics, oil & gas facilities, industrial zones, and municipal authorities are all seeking stable, efficient, and regulation-oriented thermal treatment solutions.

For project owners and contractors evaluating incinerator suppliers in Algeria, selecting a factory-level manufacturer with proven export experience, standardized designs, and flexible configurations is a critical decision factor.


Why “Incinerator Suppliers in Algeria” Is a Strategic Search Term

Procurement teams in Algeria increasingly search for incinerator suppliers in Algeria rather than generic equipment traders. The intention is clear:

  • Preference for direct factory supply

  • Demand for industrial-grade waste incinerators, not lab or pilot units

  • Need for customized configurations adapted to local operating conditions

  • Focus on automation, emission control, and long-term reliability

This trend aligns with wider North African and Mediterranean environmental policies, where waste treatment projects emphasize durability, traceability, and lifecycle cost control rather than short-term pricing.

You can explore current global search results for this topic here:
https://www.google.com/search?q=incinerator+suppliers+in+Algeria


HICLOVER: Factory-Based Waste Incinerator Manufacturer

HICLOVER is an industrial manufacturer specializing in waste incinerator systems for international markets, with extensive project references across Africa, the Middle East, and emerging economies.

Unlike trading companies or resellers, HICLOVER operates as a direct manufacturing supplier, offering:

  • Engineering-driven system design

  • Stable production standards

  • Transparent technical documentation

  • Export-oriented packing and logistics coordination

Official website: https://www.hiclover.com/


Waste Incinerator Applications Relevant to Algeria

HICLOVER incinerators are designed for a wide range of Algerian use scenarios:

  • Medical waste incinerators for hospitals and clinics

  • Industrial waste incinerators for factories, oil & gas sites, and utilities

  • Animal and veterinary waste incinerators

  • Municipal and controlled solid waste disposal

  • Emergency and remote-site incineration for desert or off-grid locations

These systems are engineered to operate reliably under high ambient temperatures, variable waste composition, and limited local infrastructure—conditions commonly encountered in Algeria.


Automation and Control: Reducing Operational Risk

Modern waste management projects demand more than simple combustion. HICLOVER incinerators integrate PLC-based automation systems to ensure:

  • Automatic temperature regulation

  • Controlled burner operation

  • Safety interlocks and alarm logic

  • Reduced operator dependency

  • Stable combustion cycles with minimal manual intervention

This automation approach directly supports Algeria’s move toward safer, standardized, and auditable waste treatment practices.


Mobile, Containerized, and Installation-Free Options

A key advantage when evaluating incinerator suppliers in Algeria is the availability of modular and mobile solutions.

HICLOVER provides:

  • Containerized incinerators (20ft / 40ft)

  • Skid-mounted and trailer-mounted systems

  • Plug-and-play, installation-free designs

  • Rapid deployment for temporary or phased projects

These solutions are particularly suitable for:

  • Remote industrial zones

  • Oil & gas camps

  • Temporary medical facilities

  • Pilot projects prior to permanent installations


Emission Control and Environmental Compliance

Environmental expectations in Algeria are evolving in line with global standards. HICLOVER waste incinerators can be configured with:

  • Dry flue gas filtration systems

  • Wet scrubbers and quench towers

  • Multi-stage gas treatment (scrubbing, neutralization, dust removal)

  • Secondary combustion chambers for complete gas oxidation

This modular emission control philosophy allows project owners to balance regulatory requirements, operational cost, and future upgrade potential.


Factory Supply Advantages Over Trading Channels

Choosing a factory-based supplier offers measurable long-term benefits:

  • Consistent quality control from design to fabrication

  • Clear responsibility for system performance

  • Easier spare parts and technical support

  • Better alignment for EPC and institutional tenders

For Algerian buyers, this translates into lower lifecycle risk and stronger project credibility.


Conclusion

For organizations searching for incinerator suppliers in Algeria, the market is shifting toward experienced manufacturers capable of delivering automated, modular, and export-ready waste incinerator systems. HICLOVER represents a factory-driven approach focused on engineering reliability, operational efficiency, and adaptability to Algerian project conditions.


Résumé en français
Les fournisseurs d’incinérateurs en Algérie privilégient de plus en plus des fabricants directs capables de proposer des incinérateurs de déchets fiables, automatisés et modulaires, adaptés aux hôpitaux, à l’industrie et aux zones isolées.

Resumen en español
Los proveedores de incineradores en Argelia buscan soluciones industriales de incineración de residuos con alto nivel de automatización, diseño modular y suministro directo de fábrica para proyectos médicos e industriales.

Mobile: +86-13813931455(WhatsApp)

Email:     [email protected]     
Email:     [email protected] 


2026-01-11/21:48:19

Pet Cremation Incinerator System (30–50 kg/h) HICLOVER TS50PET

HICLOVER TS50PET

Pet Cremation Incinerator System (30–50 kg/h)

Product Overview

The HICLOVER TS50PET Pet Cremation Incinerator is a purpose-designed, industrial-grade cremation system engineered for the dignified and environmentally responsible disposal of animal remains. Designed around proven dual-chamber incineration principles and enhanced flue-gas treatment stages, the TS50PET delivers stable high-temperature combustion, low residue generation, and reliable operation for veterinary clinics, animal hospitals, municipal animal control centers, and professional pet cremation facilities.

With flexible fuel options (diesel, natural gas, or LPG), optional wet flue-gas treatment, and multiple mobile configurations, the TS50PET adapts to diverse site conditions while maintaining consistent cremation performance and operator safety.

Waste Type & Process

Waste Type: Pet cremation (animal remains)

Treatment Method: High-temperature incineration

Target Capacity: 30–50 kg/hour

Feed Mode: Manual batch feeding

System Configuration

The TS50PET integrates a multi-stage combustion and flue-gas management layout to ensure complete oxidation and controlled emissions:

Primary Combustion Chamber
Direct cremation of animal remains under controlled high temperature.

Particulate Sedimentation and Flue Gas Retention Chamber
Reinforced gas-conditioning chamber for particulate settling and extended flue-gas residence time.

Mix Combustion Chamber
High-temperature mixing zone to enhance oxidation and stabilize gas flow before secondary treatment.

Secondary Combustion Chamber
Complete oxidation of flue gases generated from the primary chamber, ensuring destruction of odors and organic compounds.

Chimney System
6-meter stainless-steel (SS304) stack for safe and stable discharge.

Control System
PLC-based automatic control with safety interlocks, alarms, and operating logic.

Typical HICLOVER System Features

Dual-chamber incineration with extended gas residence time (≥ 2.0 seconds)

High-temperature retention (HTR) with adjustable control logic

Italy-brand burners with automatic ON/OFF operation

Intelligent fuel-saving and temperature-linked burner control

APO (Automatic Protection Operator) system for operator safety

Dry scrubber included as standard; wet scrubber available as an option

Modular design suitable for fixed or mobile deployment

Heavy-duty refractory structure for long service life

Simple operation, low maintenance, and high reliability

Pet Cremation–Dedicated Design

The TS50PET is specifically optimized for pet cremation applications:

Chamber volumes matched to animal body size for efficient heat utilization

Stable flame and temperature control to ensure respectful, complete cremation

Low ash residue (≤ 5%), easy ash handling, and movable waste/ash bed

Odor-controlled operation through secondary combustion and optional wet scrubbing

Quiet, clean, and compact layout suitable for urban or clinic environments


Key Technical Data (HICLOVER TS50PET)

Capacity & Operation

Burn Rate (Average): 20–30 kg/h

Design Capacity: 30–50 kg/h

Feed Capacity: 50–80 kg per feeding

Residency Time: ≥ 2.0 seconds

Combustion Chambers

1#Primary Chamber Volume: 560 L

2#Particulate Sedimentation & Gas Retention Chamber: 180 L

3#Mix Combustion Chamber: 50 L

4#Secondary Chamber Volume: 280 L

Temperature Range

Primary Chamber: 800–1000 °C

Secondary Chamber: 1000–1300 °C

Fuel & Consumption

Fuel Type: Diesel / Natural Gas / LPG

Diesel Consumption (Theoretical): ~14 kg/h

Natural Gas Consumption: ~16 m³n/h

Burner Configuration

Primary Chamber: G10LC single-stage burner ×1 (8 kg/h)

Secondary Chamber: G10LC single-stage burner ×1 (8 kg/h)

Electrical System

Voltage: 220 / 380 V

Power: 0.7 / 3.0 kW

Control & Safety

PLC Automatic Control

Continuous feeding protection sensors

Temperature monitoring with corundum probe tube (1600 °C rated)

Automatic cooling, alarms (display / voice / light), and system testing mode

Structure & Materials

Hot Face Refractory: ≥115 mm, 65% Al₂O₃, 1750 °C grade

Cold Face Insulation: High-grade refractory ceramic fiber

Chimney: SS304, 6 m height

External Paint: 250 °C heat-resistant coating

Dimensions & Weight

External Dimensions: 190 × 130 × 155 cm

Gross Weight: 5,000–7,000 kg

Flue Gas Treatment Options

Dry Scrubber: Included


Wet Scrubber (Optional):

First-stage stainless-steel spray tower (primary scrubber)

Second-stage stainless-steel spray tower (secondary scrubber)

Stainless-steel demister tower

Stainless-steel demisting & dust-removal filter

Integrated water tank with induced draft (ID) fan


Optional Configurations

Containerized mobile type

Trailer-mounted or sledge-mounted mobile versions

Dual-fuel (oil & gas) system

Flame observation window

Fire grate

Heat Recovery Technology (HHT)

Compliance & Manufacturing

CE compliance: 2006/42/EC, 2014/30/EU

ISO 9001:2015 certified manufacturing

No asbestos or mercury-containing materials

High-tech enterprise certification


HICLOVER TS50PET delivers a balanced combination of traditional dual-chamber incineration principles and forward-looking modular design, providing a dependable, clean, and respectful solution for modern pet cremation operations.


Mobile: +86-13813931455(WhatsApp)

Email:     [email protected]     
Email:     [email protected] 


2025-12-21/14:46:05

Incinerator Items/Model

HICLOVER TS100(PLC)


Burn Rate (Average)

100kg/hour

Feed Capacity(Average)

150kg/feeding

Control Mode

PLC Automatic

Intelligent Sensor

Continuously Feeding with Worker Protection

High Temperature Retention(HTR)

Yes (Adjustable)

Intelligent Save Fuel Function

Yes

Primary Combustion Chamber

1200Liters(1.2m3)

Internal Dimensions

120x100x100cm

Secondary Chamber

600L

Smoke Filter Chamber

Yes

Feed Mode

Manual

Burner Type

Italy Brand

Temperature Monitor

Yes

Temperature Thermometer

Corundum Probe Tube, 1400℃Rate.

Temperature Protection

Yes

Automatic Cooling

Yes

Automatic False Alarm

Yes

Automatic Protection Operator(APO)

Yes

Time Setting

Yes

Progress Display Bar

3.7 in” LCD Screen

Oil Tank

200L

Chimney Type

 Stainless Steel 304

1st. Chamber Temperature

800℃–1000℃

2nd. Chamber Temperature

1000℃-1300℃

Residency Time

2.0 Sec.

Gross Weight

7000kg

External Dimensions

270x170x190cm(Incinerator Main Body)

Burner operation

Automatic On/Off

Dry Scrubber

Optional

Wet Scrubber

Optional

Top Loading Door

Optional

Asbestos Mercury Material

None

Heat Heart Technology(HHT)

Optional

Dual Fuel Type(Oil&Gas)

Optional

Dual Control Mode(Manual/Automatic)

Optional

Temperature Record

Optional

Enhanced Temperature Thermometer

Optional

Incinerator Operator PPE Kits

Optional

Backup Spare Parts Kits

Optional

Mobile Type

Optional:Containerized/Trailer/Sledge Optional

Namibia Waste Incinerator Market Report: Market Characteristics, Demand Trends, and Suitability of Modern Incineration Technology

Namibia Waste Incinerator Market Report: Market Characteristics, Demand Trends, and Suitability of Modern Incineration Technology


1. Overview of Namibia’s Waste Management Environment
Namibia, with major cities such as Windhoek, Walvis Bay, Swakopmund, Oshakati, and Rundu, faces increasing pressures to modernize its waste-handling systems. Despite its relatively low population density, the country generates diverse waste streams due to growing healthcare services, coastal industrial activities, tourism-related operations, and expanding urban centers.

While Namibia maintains a strong environmental policy framework, the availability of compliant waste-treatment infrastructure remains limited outside Windhoek. This gap has created strong demand for engineered incineration systems capable of meeting international standards. The United Nations, UNDP, and health-sector partners contribute significantly through technical guidance, funding, and strengthening of environmental governance.

2. Key Market Characteristics
The Namibian waste-incineration market is shaped by unique structural factors:

  • High variability in waste composition, including medical, tourism-related, industrial, and community-generated waste.

  • Strong reliance on decentralized waste treatment, especially in remote regions such as Kunene, Kavango, Omaheke, and Hardap.

  • Environmental sensitivity, particularly along coastal areas like Walvis Bay and Lüderitz, where marine ecosystems require strict pollution control.

  • Infrastructure asymmetry, with rural clinics and remote outposts needing compact and easy-to-operate incinerator systems.

  • Regulatory pressure, driven by Namibia’s Ministry of Environment and supported by UN agencies focused on public health, emissions reduction, and safe disposal.

These factors shape a market that values efficiency, mobility, durability, and reliable emission-control performance.

3. Market Demand and Emerging Trends
Several trends define Namibia’s growing need for engineered incineration solutions:

  1. Expansion of healthcare infrastructure
    Hospitals and clinics in Windhoek, Oshakati, Katima Mulilo, and Keetmanshoop require reliable medical waste incinerators to meet rising service levels.

  2. Tourism and hospitality waste growth
    Coastal destinations like Swakopmund and Walvis Bay produce significant waste streams that require hygienic disposal, including food, packaging, and contaminated waste.

  3. Mining and industrial activity
    Mines in Erongo, Karas, and Kunene generate hazardous and semi-hazardous waste, creating demand for durable, high-temperature incinerators.

  4. United Nations and NGO operations
    UN agencies frequently deploy incinerator systems to strengthen emergency preparedness and improve environmental health standards in remote communities.

  5. Focus on localized treatment
    To reduce transport risks and cost, Namibia is investing in on-site waste treatment, creating strong demand for mobile and containerized incinerator systems.

4. Suitability of Incinerators for Namibia’s Local Conditions
Given Namibia’s climate, geography, and waste characteristics, suitable incinerator features include:

  • Multi-chamber high-temperature combustion for complete burnout of mixed or low-calorific waste.

  • LPG or diesel burners, ensuring stable combustion even in coastal humidity or desert wind conditions.

  • Top-loading systems, ideal for bulky community waste, tourism-sector waste, and rural health-facility operations.

  • Containerized/mobile configurations that allow installation in remote districts without extensive civil engineering.

  • Optional wet scrubbers or dry filtration in environmentally sensitive areas such as Walvis Bay and Swakopmund.

These features align with the procurement guidelines used in UN-supported projects across Southern Africa.

5. HICLOVER Incinerators: Advantages for the Namibian Market
HICLOVER provides multiple waste-incineration models well suited for Namibia’s diverse operational needs:

  • Top-loading waste incinerators suitable for municipal, tourism, and agricultural waste streams in Windhoek and Swakopmund.

  • Medical waste incinerators with secondary combustion, ideal for hospitals in Oshakati, Rundu, and Katima Mulilo.

  • Containerized mobile incinerators, preferred by UN missions, NGOs, and remote facilities for rapid deployment and reduced installation effort.

  • Optional gas-cleaning systems, strengthening compliance in protected or high-sensitivity zones.

  • Robust structural design and automated burners, ensuring reliable operation in Namibia’s extreme desert climate.

To reinforce keyword relevance, here are internal links pointing only to HICLOVER pages:

  • medical waste incinerator Namibia

  • top-loading waste incinerator

  • municipal waste incinerator system

  • containerized mobile incinerator

  • Namibia waste treatment equipment

6. Additional Highlight: Namibia’s Coastal Environmental Protection Priority
Walvis Bay, Swakopmund, Lüderitz, and other coastal zones represent some of Namibia’s most environmentally sensitive areas. Waste mismanagement in these regions can affect fisheries, tourism, and marine ecology. High-efficiency incineration, especially with optional filtration stages, plays a crucial role in preventing contamination and protecting Namibia’s iconic Atlantic coastline.

This theme is increasingly emphasized in environmental planning documents supported by the United Nations and local authorities.

7. Market Outlook
Namibia’s incinerator market is expected to grow steadily due to:

  • Continued expansion of national healthcare services

  • Strengthened environmental oversight from both government and UN partners

  • Investment in localized waste infrastructure in rural provinces

  • Increased industrial and mining activity

  • Rising tourism-sector waste generation along the coast

These conditions position Namibia as an attractive and steadily growing market for modern waste-incineration technologies.

Namibia requires waste-incineration solutions that operate reliably in varied climatic zones—from desert regions in Hardap and Omaheke to coastal cities like Walvis Bay and Lüderitz.
HICLOVER’s engineered systems, with options for mobile deployment, multi-chamber combustion, and advanced emissions control, align with Namibia’s technical, regulatory, and humanitarian needs. Their proven durability and field adaptability make them well suited for long-term national and donor-supported waste-management projects.


Kurze Zusammenfassung auf Deutsch:
Namibia zeigt einen wachsenden Bedarf an modernen Abfallverbrennungsanlagen, geprägt durch steigende medizinische Abfälle, Tourismus, Bergbau und strenge Umweltanforderungen. Städte wie Windhoek, Swakopmund und Walvis Bay benötigen zuverlässige Lösungen mit hoher Effizienz und stabiler Emissionskontrolle. HICLOVER-Incineratoren bieten robuste, anpassungsfähige und leicht installierbare Systeme, die sowohl lokalen Behörden als auch UN-Organisationen eine langfristige, konforme Entsorgung ermöglichen.

Mobile: +86-13813931455(WhatsApp)

Email:     [email protected]     
Email:     [email protected] 


2025-12-11/14:42:11

Incinerator Items/Model

HICLOVER TS100(PLC)


Burn Rate (Average)

100kg/hour

Feed Capacity(Average)

150kg/feeding

Control Mode

PLC Automatic

Intelligent Sensor

Continuously Feeding with Worker Protection

High Temperature Retention(HTR)

Yes (Adjustable)

Intelligent Save Fuel Function

Yes

Primary Combustion Chamber

1200Liters(1.2m3)

Internal Dimensions

120x100x100cm

Secondary Chamber

600L

Smoke Filter Chamber

Yes

Feed Mode

Manual

Burner Type

Italy Brand

Temperature Monitor

Yes

Temperature Thermometer

Corundum Probe Tube, 1400℃Rate.

Temperature Protection

Yes

Automatic Cooling

Yes

Automatic False Alarm

Yes

Automatic Protection Operator(APO)

Yes

Time Setting

Yes

Progress Display Bar

3.7 in” LCD Screen

Oil Tank

200L

Chimney Type

 Stainless Steel 304

1st. Chamber Temperature

800℃–1000℃

2nd. Chamber Temperature

1000℃-1300℃

Residency Time

2.0 Sec.

Gross Weight

7000kg

External Dimensions

270x170x190cm(Incinerator Main Body)

Burner operation

Automatic On/Off

Dry Scrubber

Optional

Wet Scrubber

Optional

Top Loading Door

Optional

Asbestos Mercury Material

None

Heat Heart Technology(HHT)

Optional

Dual Fuel Type(Oil&Gas)

Optional

Dual Control Mode(Manual/Automatic)

Optional

Temperature Record

Optional

Enhanced Temperature Thermometer

Optional

Incinerator Operator PPE Kits

Optional

Backup Spare Parts Kits

Optional

Mobile Type

Optional:Containerized/Trailer/Sledge Optional

Global Market Landscape for Small-Scale Medical Waste Incinerators

Global Market Landscape for Small-Scale Medical Waste Incinerators


The safe disposal of medical and hazardous waste is a critical concern worldwide, driving demand for effective on-site incineration solutions. Small-scale waste incinerators C especially those designed for medical waste C have emerged as essential tools in remote clinics, disaster zones, and underserved healthcare facilities where conventional waste management infrastructure is lacking. In fact, as of 2021 only about 61% of hospitals worldwide had basic healthcare waste services, dropping to just 25% in fragile regions[1]. This gap underlines why on-site incineration is often relied upon as an immediate solution. International bodies like the United Nations (UN) and World Health Organization (WHO) play a key role in promoting these technologies through guidelines and support programs. This has made small incinerators a focal point for government agencies, humanitarian NGOs, healthcare providers, and environmental organizations looking to protect public health and the environment.


Global Market Trends and Landscape


Globally, the market for small-scale incinerators is on a steady growth trajectory. In 2024 the small waste incinerator sector was valued around $2.5 billion and is projected to reach roughly $5.0 billion by 2034, with a robust ~7% annual growth rate[2]. This expansion is propelled by increasing urbanization and stringent waste regulations in many countries that demand safer disposal methods[3]. Small-scale incinerators (units handling less than about 1 ton per hour) make up a significant share C roughly 40% of the overall incinerator market C reflecting their suitability for localized applications[4]. The Asia-Pacific region currently leads in adoption, accounting for about 45% of global revenue as rapidly developing nations invest in waste management infrastructure[5]. Meanwhile, emerging markets in Africa and Latin America are also seeing rising demand, driven by healthcare expansion and the need to replace unsafe practices like open burning.

Key drivers behind this trend include heightened environmental awareness and the push for sustainable waste solutions. Governments are tightening rules on medical and hazardous waste disposal, often requiring modern incineration (or equivalent treatment) to prevent pollution. At the same time, industries and municipalities seek to reduce reliance on overcrowded landfills by using compact incinerators that significantly reduce waste volume and eliminate pathogens on-site. Technological advances C such as automated controls and emissions monitoring C are making new incinerator models more efficient and easier to operate, which further encourages adoption. However, the market does face challenges: high initial costs and strict permitting processes can slow deployment in some regions[6]. Even so, the overall outlook remains positive as public health needs and environmental safeguards align in favor of safe, small-scale incineration as part of comprehensive waste management.

Mobile: +86-13813931455(WhatsApp)

Email:     [email protected]     
Email:     [email protected] 


2025-12-11/10:30:20

Incinerator Items/Model

HICLOVER TS100(PLC)


Burn Rate (Average)

100kg/hour

Feed Capacity(Average)

150kg/feeding

Control Mode

PLC Automatic

Intelligent Sensor

Continuously Feeding with Worker Protection

High Temperature Retention(HTR)

Yes (Adjustable)

Intelligent Save Fuel Function

Yes

Primary Combustion Chamber

1200Liters(1.2m3)

Internal Dimensions

120x100x100cm

Secondary Chamber

600L

Smoke Filter Chamber

Yes

Feed Mode

Manual

Burner Type

Italy Brand

Temperature Monitor

Yes

Temperature Thermometer

Corundum Probe Tube, 1400℃Rate.

Temperature Protection

Yes

Automatic Cooling

Yes

Automatic False Alarm

Yes

Automatic Protection Operator(APO)

Yes

Time Setting

Yes

Progress Display Bar

3.7 in” LCD Screen

Oil Tank

200L

Chimney Type

 Stainless Steel 304

1st. Chamber Temperature

800℃–1000℃

2nd. Chamber Temperature

1000℃-1300℃

Residency Time

2.0 Sec.

Gross Weight

7000kg

External Dimensions

270x170x190cm(Incinerator Main Body)

Burner operation

Automatic On/Off

Dry Scrubber

Optional

Wet Scrubber

Optional

Top Loading Door

Optional

Asbestos Mercury Material

None

Heat Heart Technology(HHT)

Optional

Dual Fuel Type(Oil&Gas)

Optional

Dual Control Mode(Manual/Automatic)

Optional

Temperature Record

Optional

Enhanced Temperature Thermometer

Optional

Incinerator Operator PPE Kits

Optional

Backup Spare Parts Kits

Optional

Mobile Type

Optional:Containerized/Trailer/Sledge Optional

Incinérateurs HICLOVER à Petit Volume — Présentation des Modèles à Chargement Supérieur TS10, TS20 et TS30

Incinérateurs HICLOVER à Petit Volume — Présentation des Modèles à Chargement Supérieur TS10, TS20 et TS30

Les HICLOVER TS10, TS20 et TS30 constituent une gamme compacte et robuste d’incinérateurs à chargement supérieur (porte supérieure) spécialement développée pour les installations ayant de faibles volumes de déchets au quotidien. Grâce à leur conception verticale, ces modèles conviennent parfaitement aux cliniques rurales, fermes, laboratoires, équipes mobiles et sites temporaires, où la simplicité, la sécurité et l’efficacité sont essentielles pour traiter les déchets solides légers, les résidus biologiques, les petites carcasses animales et divers déchets non dangereux.


1. Pourquoi le Chargement Supérieur est un Atout Essentiel

L’élément central des modèles TS10 / TS20 / TS30 est la porte supérieure, permettant d’introduire les déchets directement par le dessus de la chambre primaire. Cette configuration offre plusieurs avantages opérationnels :

  • Chargement facilité par la gravité, particulièrement utile pour les déchets légers ou irréguliers

  • Moins de pertes de chaleur lorsque la porte est ouverte

  • Processus de travail simplifié, sans pousser ni compresser les déchets

  • Maniabilité accrue dans les zones étroites ou les sites improvisés

  • Moindre exposition de l’opérateur aux gaz chauds ou aux flammes

Pour les faibles volumes de déchets, le chargement vertical garantit une préparation rapide, des manipulations réduites et une utilisation intuitive, adaptée même aux utilisateurs non spécialisés.


2. Présentation des Modèles TS10, TS20 et TS30

Bien qu’appartenant à la même famille, chaque modèle répond à un besoin de capacité différent. La cohérence d’ingénierie assure une performance stable sur toute la série.

TS10 – Incinérateur Ultra-Compact à Chargement Supérieur

  • Volume de la chambre primaire : environ 110 litres

  • Capacité typique par cycle : 8–10 kg

  • Brûleur : Riello FS10 (diesel, fabrication italienne)

  • Température de la chambre primaire : 800–900°C

  • Température de la chambre secondaire : 1000–1200°C

  • Usage idéal : petites cliniques, mini-laboratoires, unités vétérinaires, solutions mobiles

TS20 – Modèle Standard pour Petites Installations

  • Volume de la chambre primaire : 220 litres

  • Capacité par cycle : 15–20 kg

  • Brûleur : Riello FS10, selon le type de carburant

  • Températures typiques : similaires au TS10, adapté aux cycles continus

  • Usage idéal : cliniques rurales, stations de recherche, petites fermes, camps humanitaires

TS30 – Unité Renforcée à Petite Capacité

  • Volume de la chambre primaire : 330 litres

  • Capacité par cycle : 25–30 kg

  • Brûleur : Riello FS10 (diesel ou gaz)

  • Hauteur de chambre augmentée pour recevoir des charges plus volumineuses

  • Usage idéal : centres de santé régionaux, hôpitaux de campagne, élevages avicoles, communautés isolées

Dans les trois modèles, la porte supérieure permet une introduction directe des déchets comme le papier, les emballages plastiques, les déchets médicaux légers ou les petites carcasses.


3. Fonctionnalités Techniques Essentielles des Incinérateurs HICLOVER

Tous les incinérateurs HICLOVER à chargement supérieur sont conçus sur une base technique solide destinée à un fonctionnement durable :

  • Double chambre de combustion avec post-combustion des gaz

  • Affichage numérique ou PLC pour le contrôle des températures et des brûleurs

  • Briques réfractaires et isolants haute performance

  • Thermocouples pour la surveillance des deux chambres

  • Allumage automatique et contrôle de flamme

  • Compatibilité diesel, LPG ou gaz naturel

  • Cheminées en acier inoxydable, avec option de laveur humide

  • Faible exigence d’installation, idéal pour les déploiements rapides

Ces caractéristiques assurent des cycles de combustion réguliers, des émissions plus propres et un entretien minimal, ce qui est essentiel pour les sites éloignés ou limités en ressources.


4. Options de Déploiement Mobile

Les séries TS10 / TS20 / TS30 sont particulièrement adaptées aux missions mobiles, ce qui en fait un choix privilégié pour les ONG, les opérations d’urgence ou les laboratoires de terrain.

Version sur Remorque

Utilisée par les services vétérinaires, équipes médicales rurales et unités d’inspection.

Incinérateur Mobile en Conteneur

Intégré dans un conteneur 20 pieds, équipé de sorties de cheminée, d’aération, d’éclairage et de réservoirs optionnels. Idéal pour les missions de l’ONU, camps de réfugiés ou sites industriels éloignés.

Montage sur Skid

Facilement déplacé par chariot élévateur au sein d’usines, chantiers miniers, zones agricoles ou de construction.

Unité de Déploiement Rapide

Solution légère, conçue pour les camps médicaux d’urgence, les zones d’épidémie et les laboratoires mobiles.

Le chargement supérieur reste efficace dans toutes ces configurations car l’accès vertical ne dépend pas des conditions du sol.


5. Applications Étendues dans Divers Secteurs

Déchets Médicaux (Petites Structures de Santé)

Gestion des déchets :

  • déchets infectieux, EPI, pansements

  • déchets cliniques légers (coton, papier, petites seringues)

  • flux de déchets typiques des cliniques rurales

Secteur Vétérinaire et Avicole

Chargement facile via la porte supérieure pour :

  • petites carcasses

  • sous-produits avicoles

  • litières ou emballages contaminés

Laboratoires de Recherche

Élimination sécurisée de :

  • échantillons biologiques

  • boîtes de culture

  • papier et emballages contaminés

Camps Humanitaires et Missions de Terrain

Adapté aux besoins des :

  • camps de réfugiés

  • bases de missions ONU

  • équipes médicales mobiles

  • unités d’intervention d’urgence

Usage Commercial et Industriel Léger

Convient aux :

  • ateliers, petites usines

  • hôtels, lodges, éco-hébergements

  • sites isolés nécessitant une élimination quotidienne des déchets légers


6. Pourquoi la Série TS10 / TS20 / TS30 se Distingue

La gamme d’incinérateurs HICLOVER à petite capacité est reconnue pour :

  • son utilisation simple grâce à la porte supérieure

  • ses températures stables de combustion (jusqu’à 1200°C)

  • sa faible consommation de carburant

  • son format compact, adapté en intérieur ou extérieur

  • sa compatibilité élevée avec les solutions mobiles

  • sa construction robuste pour un usage prolongé

Ces atouts font de la série TS10 / TS20 / TS30 un choix idéal pour toute organisation recherchant un incinérateur à chargement supérieur fiable, compact et performant, capable de fonctionner efficacement dans des conditions réelles exigeantes.


Mobile: +86-13813931455(WhatsApp)

Email:     [email protected]     
Email:     [email protected] 


2025-11-24/12:40:41

Incinerator Items/Model

HICLOVER TS100(PLC)


Burn Rate (Average)

100kg/hour

Feed Capacity(Average)

150kg/feeding

Control Mode

PLC Automatic

Intelligent Sensor

Continuously Feeding with Worker Protection

High Temperature Retention(HTR)

Yes (Adjustable)

Intelligent Save Fuel Function

Yes

Primary Combustion Chamber

1200Liters(1.2m3)

Internal Dimensions

120x100x100cm

Secondary Chamber

600L

Smoke Filter Chamber

Yes

Feed Mode

Manual

Burner Type

Italy Brand

Temperature Monitor

Yes

Temperature Thermometer

Corundum Probe Tube, 1400℃Rate.

Temperature Protection

Yes

Automatic Cooling

Yes

Automatic False Alarm

Yes

Automatic Protection Operator(APO)

Yes

Time Setting

Yes

Progress Display Bar

3.7 in” LCD Screen

Oil Tank

200L

Chimney Type

 Stainless Steel 304

1st. Chamber Temperature

800℃–1000℃

2nd. Chamber Temperature

1000℃-1300℃

Residency Time

2.0 Sec.

Gross Weight

7000kg

External Dimensions

270x170x190cm(Incinerator Main Body)

Burner operation

Automatic On/Off

Dry Scrubber

Optional

Wet Scrubber

Optional

Top Loading Door

Optional

Asbestos Mercury Material

None

Heat Heart Technology(HHT)

Optional

Dual Fuel Type(Oil&Gas)

Optional

Dual Control Mode(Manual/Automatic)

Optional

Temperature Record

Optional

Enhanced Temperature Thermometer

Optional

Incinerator Operator PPE Kits

Optional

Backup Spare Parts Kits

Optional

Mobile Type

Optional:Containerized/Trailer/Sledge Optional